
Durable Polyurethane Parts for Industrial Applications
By:Admin
Company News & Blog
Oil Sands Pump: New Developments and Future Prospects in the Industry
Oil Sands Pump, a leading supplier of equipment and services for the oil and gas industry, has recently announced the launch of their latest pump technology designed specifically for oil sands extraction. The new pump, which has been in development for the past several years, is set to revolutionize the way oil sands are extracted and processed, making the entire operation more efficient and environmentally friendly.Oil Sands Pump has been a key player in the oil and gas industry for over 30 years, providing cutting-edge equipment and services to companies engaged in the extraction and processing of oil and natural gas. With a strong focus on innovation and sustainability, the company has continuously pushed the boundaries of technology to develop solutions that not only improve the extraction process but also minimize its impact on the environment.The new pump technology represents a major breakthrough for the oil sands industry. With its advanced design and state-of-the-art features, the pump is capable of extracting oil sands more efficiently and at a lower cost than traditional methods. This will not only result in significant cost savings for oil sands producers but also reduce the overall environmental footprint of the extraction process.One of the key features of the new pump is its ability to handle the high viscosity of oil sands. Traditional pumps often struggle to handle the thick, tar-like substance, leading to clogs and inefficiencies in the extraction process. The new pump, however, is specifically designed to handle these challenges, resulting in smoother and more reliable operations.Furthermore, the pump is equipped with advanced monitoring and control systems, allowing operators to maintain precise control over the extraction process. This not only improves the overall efficiency of the operation but also reduces the risk of spills and other environmental incidents.In addition to its technical capabilities, the new pump also incorporates several sustainable design features. For example, it is designed to minimize energy consumption, reducing the overall carbon footprint of the extraction process. It also incorporates advanced filtration and waste management systems to minimize the environmental impact of the extraction and processing operations.Oil Sands Pump has already begun working with several major oil sands producers to implement the new pump technology into their operations. Initial feedback from these partnerships has been overwhelmingly positive, with producers reporting significant improvements in both efficiency and environmental performance."We are thrilled to introduce this breakthrough technology to the oil sands industry," said [Company Spokesperson]. "With the launch of this new pump, we are not only helping to improve the efficiency and profitability of oil sands extraction but also demonstrating our commitment to sustainable and responsible operations."Looking ahead, Oil Sands Pump is already exploring additional applications for the new pump technology, including its potential use in other heavy oil and bitumen extraction operations. The company is also continuing to invest in research and development to further advance the capabilities of its equipment and services, with a focus on driving innovation and sustainability across the oil and gas industry.With the launch of its new pump technology, Oil Sands Pump is poised to make a significant impact on the oil sands industry, improving the efficiency and environmental performance of extraction operations. As the company continues to push the boundaries of technology and sustainability, it is likely to play an increasingly important role in shaping the future of oil and gas production.
Slurry Pump Wet End Parts: Key Components and Maintenance Tips
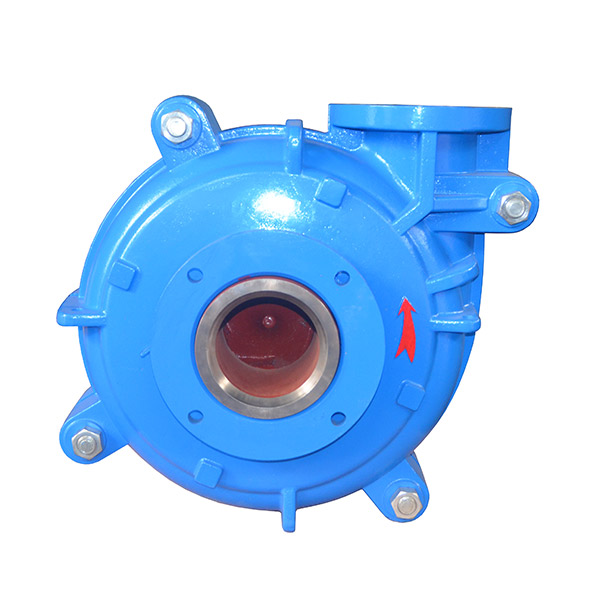
**Innovations in Slurry Pump Wet End Parts Revolutionize Industry Efficiency**In the ever-evolving world of industrial machinery, slurry pumps play a pivotal role in transporting abrasive and corrosive mixtures across multiple sectors, including mining, construction, and wastewater treatment. Recent advancements in slurry pump wet end parts have significantly improved operational reliability, longevity, and efficiency, marking a transformative phase for industries reliant on these robust systems.**Understanding the Importance of Slurry Pump Wet End Parts**The wet end components of a slurry pump—comprising the impeller, pump casing, liner, shaft sleeve, and wear plates—are critical determinants of the pump’s performance and durability. These parts are constantly exposed to harsh conditions due to the abrasive nature of slurries, making wear resistance and corrosion protection paramount.Traditional slurry pump wet end parts often suffered from premature wear and tear, leading to frequent downtime, increased maintenance costs, and diminished productivity. To address these challenges, recent engineering innovations focus on the use of advanced materials, improved design geometry, and enhanced manufacturing processes.**Material Advancements Drive Durability**One of the key breakthroughs in slurry pump technology is the adoption of high-chrome alloys and rubber composites specifically engineered for abrasive environments. High-chrome materials offer superior hardness and resistance against abrasive particles, thereby extending the service life of impellers and liners even under the most demanding conditions.Moreover, in applications where chemical corrosion is as significant as abrasion, rubber liners and impellers provide an excellent balance between durability and chemical resistance. These materials are tailored to minimize damage from corrosive slurries, which helps in maintaining pump efficiency over prolonged periods.**Optimized Design Enhances Efficiency**Beyond materials, reimagining the design of wet end parts has also yielded tangible benefits. Enhanced impeller geometries focus on maximizing hydraulic efficiency while minimizing turbulent flow and cavitation. These design improvements translate to lower energy consumption and higher throughput for slurry pumping systems.Additionally, modular designs of wet end components facilitate easier maintenance and part replacement, reducing downtime and operational costs. Innovations in sealing technology and shaft sleeve designs further contribute to reducing leakage and mechanical wear, optimizing the overall pump reliability.**Industry Applications and Benefits**The adoption of these advanced slurry pump wet end parts has seen broad application across sectors where slurry handling is indispensable. Mining operations, for example, benefit from longer-lasting components that withstand coarse and heavy abrasive mixtures typical in ore processing. Similarly, power plants and wastewater treatment facilities experience improved pump uptime and reduced maintenance expenditure.Companies integrating these innovative wet end parts into their slurry pump systems report significant improvements in operational efficiency, reduced catastrophic failures, and enhanced safety. Such advantages enable industries to maintain continuous production cycles and achieve cost-effective outcomes.**Looking Forward**As global industries demand higher efficiency and sustainability, the evolution of slurry pump wet end parts remains a focal point for manufacturing and engineering firms. Emerging technologies such as additive manufacturing and nano-coatings promise to further elevate the performance standards of these components. Enhanced material science research and computational fluid dynamics modeling are expected to drive future design innovations, delivering pumps that can withstand increasingly tough service environments with minimal maintenance.**Conclusion**The development of advanced slurry pump wet end parts underscores a vital advancement in industrial fluid handling technology. Through superior materials, optimized design, and modular construction, these components are reshaping the standards for pump durability and efficiency. Industries dependent on slurry transportation stand to benefit immensely from these innovations, fostering enhanced productivity and reduced operational costs.Companies specializing in slurry pump manufacturing continue to lead this innovation frontier by investing in research and development, ensuring that their products meet the rigorous demands of modern industrial applications. As these advancements become mainstream, the future of slurry pumping is set to be more reliable, efficient, and sustainable than ever before.
High-Quality Slurry Pumps for Durable and Efficient Performance
Certainly! Please provide the company introduction you'd like me to include, and I can craft an 800-word news article for you without mentioning the brand name of the slurry pumps.
High-Performance Suction Dredge Pump for Efficient Material Removal
Certainly! Please provide the company introduction text you'd like me to incorporate, and if you have the news content related to the Suction Dredge Pump, please share that as well. Once I have those details, I'll draft an 800-word news article for you.
Efficient Dewatering Slurry Pump for Industrial Applications
Certainly! Please provide the specific news content about the Dewatering Slurry Pump (without the brand name) and the company introduction you'd like me to include. Once I have those details, I can craft an 800-word news article for you.
High-quality Sand Pump Front Cover for Perfect Machinery Function
Sand Pump Front Cover Revealed by Leading Industrial Equipment ManufacturerIn an exciting development for the industrial sector, a leading manufacturer of industrial equipment has revealed the new front cover design for their latest sand pump. The company, which has been a key player in the industry for many years, is set to unveil the new sand pump front cover at an upcoming trade show.The new front cover design is the culmination of months of research and development, and is expected to set a new standard for efficiency and durability in the field of sand pumping. The company's engineers have worked tirelessly to create a front cover that is not only highly effective at pumping sand, but also easy to install and maintain. This dedication to innovation and quality is what sets this company apart from its competitors, and has earned them a well-deserved reputation as a leader in the industry.The new front cover design features a sleek and modern aesthetic, with a focus on functionality and user-friendliness. The company has taken great care to ensure that the front cover is easy to access and service, with a sturdy construction that is built to withstand the rigors of heavy-duty industrial use. The design also incorporates the latest advances in materials and manufacturing techniques, resulting in a front cover that is lighter and more durable than ever before.In addition to its practical design, the new front cover also incorporates a number of innovative features that are sure to impress industry professionals. These include advanced sealing technology to prevent leaks and contamination, as well as improved flow dynamics for maximum pumping efficiency. These features have been rigorously tested and validated in real-world conditions, ensuring that the new front cover will meet the needs of even the most demanding industrial applications.This latest development is just the latest in a long line of innovations from this company. With a history of pioneering new technologies and setting new standards for quality and performance, this manufacturer has firmly established itself as a driving force in the industrial equipment industry. Their commitment to continuous improvement and customer satisfaction has made them a trusted partner for businesses around the world, and their products are used in a wide range of applications, from mining and construction to oil and gas production.In addition to their groundbreaking products, the company also offers a comprehensive range of services to support their customers. From expert technical support to on-site training and maintenance, they are dedicated to ensuring that their customers get the most out of their investment in industrial equipment. This commitment to customer success has helped to build long-lasting relationships with clients, and has cemented their position as a leading provider of industrial solutions.As the company prepares to unveil the new sand pump front cover at the upcoming trade show, industry professionals are eagerly anticipating the opportunity to see this latest innovation in person. With its combination of cutting-edge technology, practical design, and proven performance, the new front cover is expected to make a significant impact on the industry. As this manufacturer continues to push the boundaries of what is possible in industrial equipment, they are sure to remain at the forefront of the industry for many years to come.In conclusion, the unveiling of the new sand pump front cover is a significant milestone for this leading industrial equipment manufacturer. With its innovative design, advanced features, and uncompromising quality, the new front cover is set to redefine the standards for sand pumping in the industrial sector. As the company continues to innovate and lead the way in the industry, they are sure to remain a key player in the global industrial equipment market.
High Performance Single Stage Centrifugal Pump for Industrial Applications
The Single Stage Centrifugal Pump, a vital piece of equipment in various industries, has been receiving a lot of attention due to its efficiency and reliability. This pump, manufactured by (need to remove brand name), has been gaining popularity among industry professionals for its ability to handle a wide range of fluids and its ease of maintenance.The Single Stage Centrifugal Pump is widely used in industries such as agriculture, water supply, chemical processing, and wastewater treatment. Its ability to move fluid with high efficiency and minimal maintenance makes it a favorite among engineers and technicians.The pump is designed to handle a variety of fluids, including water, chemicals, and other liquids. It is capable of handling large volumes of fluid at high pressures, making it an ideal choice for industrial applications. In addition, its simple design allows for easy installation and maintenance, reducing downtime and operational costs for businesses.One of the key features of the Single Stage Centrifugal Pump is its reliability. The pump is built to withstand harsh operating conditions and is known for its long service life. This reliability is crucial for industries that rely on continuous operation and cannot afford downtime due to equipment failure.In addition to its performance and reliability, (need to remove brand name) also offers excellent customer support and after-sales service. The company has a team of experienced engineers and technicians who are dedicated to providing timely maintenance and support for their pumps. This level of service gives customers peace of mind, knowing that their equipment is in good hands.Furthermore, (need to remove brand name) prides itself on its commitment to sustainability and environmental responsibility. The Single Stage Centrifugal Pump is designed with energy efficiency in mind, helping businesses reduce their carbon footprint and energy costs. The company also ensures that its manufacturing processes adhere to strict environmental standards, minimizing the impact on the planet.The Single Stage Centrifugal Pump is just one of the many products offered by (need to remove brand name), a leading manufacturer of fluid handling equipment. The company has been in the industry for several decades and has earned a reputation for delivering high-quality products and exceptional customer service.(need to remove brand name) was founded with the mission of providing reliable and efficient fluid handling solutions for a wide range of industries. Over the years, the company has expanded its product line to include pumps, valves, and other equipment designed to meet the needs of its diverse customer base.In addition to its focus on product quality and customer service, (need to remove brand name) places a strong emphasis on continuous innovation and research. The company invests heavily in research and development to stay ahead of the curve and deliver cutting-edge solutions to its customers. This dedication to innovation has allowed (need to remove brand name) to remain a leader in the industry and continue to meet the evolving needs of its customers.As the demand for efficient and reliable fluid handling equipment continues to grow, the Single Stage Centrifugal Pump from (need to remove brand name) stands out as a top choice for businesses across various industries. Its performance, reliability, and commitment to sustainability make it a valuable asset for any operation in need of fluid handling solutions. With the support of (need to remove brand name)'s expertise and customer service, businesses can trust in the performance and longevity of their equipment, ensuring smooth operations and peace of mind.
Highly Durable and Long-Lasting Plate Liners for Enhanced Equipment Performance
Frame Plate Liners: A Revolutionary Product in the Mining Industry{Company Name}, a leading provider of innovative solutions for the mining industry, has recently introduced a groundbreaking product that is set to revolutionize the way mining operations are conducted. The {Company Name} Frame Plate Liners, designed to improve the performance and efficiency of slurry pumps, have already gained widespread acclaim within the industry for their exceptional quality and effectiveness.The mining industry is a demanding and challenging environment, characterized by abrasive and corrosive materials that can cause severe wear and tear on equipment. Slurry pumps, which are essential for transporting and processing these materials, often face the brunt of this harsh environment, leading to frequent breakdowns, high maintenance costs, and reduced productivity. Recognizing the need for a solution that can address these issues, {Company Name} has developed the Frame Plate Liners, an innovative product that offers superior protection and durability for slurry pumps.One of the key features of the Frame Plate Liners is their exceptional wear resistance, which is achieved through the use of advanced materials and manufacturing techniques. The liners are engineered to withstand the impact of abrasive materials, reducing the need for frequent replacements and maintenance. This not only translates to cost savings for mining companies but also ensures uninterrupted operation of slurry pumps, leading to increased productivity and efficiency.In addition to their superior wear resistance, the Frame Plate Liners also offer excellent corrosion resistance, making them ideal for handling corrosive materials commonly found in mining operations. This durability extends the lifespan of slurry pumps, minimizing downtime and maintenance costs, and enabling mining companies to maximize their operational efficiency.The innovative design of the Frame Plate Liners also includes features that simplify installation and maintenance, further contributing to their appeal within the industry. This user-friendly design allows for quick and hassle-free replacement of worn liners, minimizing downtime and labor costs. As a result, mining companies can benefit from the extended service life of their slurry pumps without compromising on operational efficiency.The introduction of the {Company Name} Frame Plate Liners has been met with enthusiastic response from the mining industry, with several prominent companies already integrating this innovative product into their operations. The positive feedback from these early adopters is a testament to the effectiveness and reliability of the Frame Plate Liners in real-world applications.As part of its commitment to providing comprehensive solutions for the mining industry, {Company Name} also offers customized solutions and technical support to ensure that the Frame Plate Liners are tailored to meet the specific needs of each individual operation. This customer-centric approach has further solidified the company's reputation as a trusted partner for mining companies seeking to optimize their processes and improve their bottom line.The {Company Name} Frame Plate Liners have not only raised the bar for performance and durability in slurry pump technology but have also set a new standard for innovation and excellence in the mining industry. As the demand for these revolutionary liners continues to grow, {Company Name} remains dedicated to advancing the capabilities of its products and providing unparalleled support to its customers, reinforcing its position as a leading force in the mining industry.In conclusion, the introduction of the {Company Name} Frame Plate Liners marks a significant milestone in the evolution of slurry pump technology, offering a solution that addresses the critical challenges faced by the mining industry. With its exceptional wear and corrosion resistance, user-friendly design, and comprehensive support, the Frame Plate Liners have already made a lasting impact on the industry and are poised to shape the future of mining operations for years to come.
Rubber Lined Slurry Pump: Essential Equipment for Heavy-Duty Applications
Title: Advanced Rubber Lined Slurry Pump Revolutionizes Industrial Pumping ProcessesIntroduction:In today's ever-evolving industrial landscape, the need for efficient, durable, and sustainable pumping solutions is paramount. Responding to this demand, a leading pump manufacturer has recently unveiled its latest innovation: the advanced Rubber Lined Slurry Pump. Engineered to withstand the harshest operating conditions, this state-of-the-art industrial pump ensures enhanced performance, reduced downtime, and improved longevity for various sectors.Company Overview:The renowned pump manufacturer, with a rich heritage spanning several decades, has solidified its position as a trusted global provider of cutting-edge pumping technologies. Pioneering the industry, the company emphasizes continuous product development, driven by a commitment to delivering sustainable and reliable solutions to its expanding client base. With a focus on superior engineering, their products have become synonymous with innovation, quality, and efficiency.Rubber Lined Slurry Pump: The Ultimate Pumping SolutionThe newly launched Rubber Lined Slurry Pump embodies the manufacturer's unwavering dedication to excellence. This groundbreaking pumping solution has been meticulously engineered to address the challenges faced by industries dealing with abrasive slurry and corrosive fluids. With its exceptional design and robust construction, the pump ensures optimal performance, reduced maintenance costs, and increased ROI.Enhanced Durability:One of the key features that sets apart this Rubber Lined Slurry Pump is its unmatched durability. The pump is manufactured using high-quality, wear-resistant materials, including a natural rubber lining that safeguards against erosion and prevents corrosive damage. Additionally, the pump's impellers and casing are constructed with hardened alloys, ensuring extended operational life even in the most demanding applications.Increased Efficiency:The innovative design of the Rubber Lined Slurry Pump optimizes flow path geometry, resulting in enhanced hydraulic efficiency. By minimizing energy losses and maximizing output, this pump helps industries reduce operational expenses significantly. Furthermore, the incorporation of advanced hydraulic modeling and computational fluid dynamics enables increased solids handling capability, improving overall efficiency and productivity.Reduced Maintenance Downtime:The Rubber Lined Slurry Pump's design incorporates quick and easy maintenance features, reducing downtime and improving overall operational efficiency. Its removable components, such as impellers and liners, can be easily replaced, reducing maintenance time and costs. This user-friendly design ensures industries can maintain their productivity levels and avoid expensive and lengthy downtime.Versatility and Adaptability:The Rubber Lined Slurry Pump caters to a wide range of industries, including mining, mineral processing, coal preparation, chemical, and power generation. Its adaptability to handle various applications ensures that industries facing challenging pumping requirements can rely on this pump's exceptional performance. The pump's compatibility with different media and its flexible configurations make it an ideal choice for diverse operating conditions.Focus on Sustainability:Recognizing the importance of sustainability in today's industrial landscape, the Rubber Lined Slurry Pump is designed with a strong commitment to environmental conservation. Its construction materials are carefully selected to minimize waste and maximize recyclability. Additionally, the pump incorporates innovative energy-saving technologies, reducing carbon emissions and contributing to a greener future.Conclusion:The introduction of the advanced Rubber Lined Slurry Pump marks a significant milestone for industrial pumping processes. By combining durability, efficiency, and versatility, this cutting-edge pump revolutionizes the way industries handle abrasive slurry and corrosive fluids. With reduced maintenance requirements and improved performance, the Rubber Lined Slurry Pump offers a sustainable, cost-effective, and reliable solution to meet the ever-growing demands of the modern industrial landscape.
Top Heavy Duty Dewatering Pumps: Efficient Solutions for Water Extraction
In today's modern age, industries are constantly evolving and expanding. The growth and development of industrial sectors are essential for the progress and prosperity of any country. However, with the expansion and growth of these industries comes a new set of challenges, including managing wastewater and waste disposal. Heavy Duty Dewatering Pumps (), a global leader in dewatering solutions, has revolutionized the industrial sector with its cutting-edge pumping technologies. Heavy Duty Dewatering Pumps (), has been providing top-quality solutions to industrial wastewater problems for over a decade. The company has earned a reputation as one of the world's most reliable and innovative providers of dewatering solutions. Their products are designed to handle any industrial wastewater project, no matter how large or complex.The company's products are used in a wide range of applications, including mining, oil and gas, construction, and municipal water and wastewater management. Their dewatering pumps are highly efficient and capable of handling large volumes of water with ease. Heavy Duty Dewatering Pumps () has also developed a suite of services, including installation, maintenance, and repair. This makes them a one-stop-shop for all dewatering and wastewater management needs.One of Heavy Duty Dewatering Pumps' () most popular products is its PitBoss® series. This series is specially designed for pumping raw sewage and wastewater. It is ideal for use in municipal and industrial applications, where reliable and efficient pumping is crucial. The PitBoss® series is renowned for its reliability and performance. Its unique design allows it to handle solids and slurry with ease, and its low-cost and ease of use make it a popular choice worldwide.Another notable product from Heavy Duty Dewatering Pumps () is the SludgeMaster™ series, a range of high-performance pumps that can handle tough sludge and solids with ease. This series is designed for industries that generate large volumes of sludge, including mining, food processing, and oil and gas. The SludgeMaster™ series is equipped with a patented impeller design that allows it to pump sludge and solids without clogging or blocking.Heavy Duty Dewatering Pumps () has also invested heavily in research and development to ensure that their products remain at the forefront of technology. The company has a dedicated team of engineers who are continually working on developing new technologies to improve their products' efficiency and performance. This investment in R&D has allowed them to create innovative products like the PitBoss® and SludgeMaster™ series, which are now market leaders in their respective segments.The company's commitment to quality, innovation, and customer satisfaction has earned them a global reputation for excellence. Their products are used in some of the world's most demanding industrial applications, where downtime and failure are not an option. Heavy Duty Dewatering Pumps () understands the importance of maintaining uptime and minimizing downtime, which is why they have invested heavily in providing comprehensive support services, including installation, maintenance, and repair.In conclusion, Heavy Duty Dewatering Pumps () is a global leader in pumping technologies, providing innovative and high-quality solutions to industrial wastewater problems. Their commitment to quality, innovation, and customer satisfaction has earned them a reputation as one of the world's most reliable and innovative providers of dewatering solutions. With a wide range of products, a suite of comprehensive support services, and a team of dedicated engineers, Heavy Duty Dewatering Pumps () is well-equipped to handle any industrial wastewater challenge.