Efficient Dewatering Pumps for Mining Applications

By:Admin
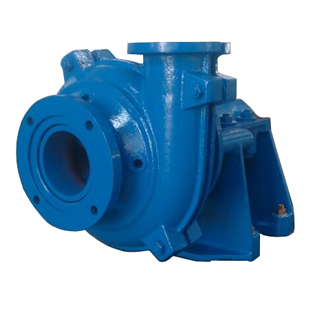
Horizontal Metal Lined Light Duty Slurry Pump SL/100D
**Innovations in Dewatering Pumps Revolutionize the Mining Industry**

In the dynamic landscape of mining operations, efficient water management remains a critical challenge. Dewatering pumps, essential for extracting water from mine sites, have witnessed significant technological advancements that are transforming mining efficiency and safety. Recent developments in dewatering pump technology have propelled the mining industry towards more sustainable, cost-effective, and reliable solutions.

Dewatering pumps play a pivotal role in mining by removing excess water from shafts, pits, and trenches. This process is fundamental to maintain dry working conditions, prevent flooding, and ensure the structural integrity of mining sites. Traditionally, the industry has grappled with issues such as high energy consumption, frequent maintenance, and limited adaptability of pumps to various mining environments.

Leading companies in the pump manufacturing sector have responded by integrating innovative design features and materials into their dewatering pump solutions. These innovations include enhanced wear resistance, improved hydraulic performance, and the incorporation of automation and remote control capabilities. Such features not only extend the lifespan of pumps but also optimize performance, reducing downtime and operational costs.

The impact of advanced dewatering pumps is particularly notable in the context of large-scale mining projects where water inflow can be substantial. Efficient pumps enable continuous operation, minimizing the risk of delays caused by water-related disruptions. Moreover, with increasing environmental regulations, the ability to precisely control dewatering processes supports compliance efforts while mitigating the ecological footprint.

One company at the forefront of these advancements is renowned for its commitment to engineering excellence and customer-centric solutions. With a strong emphasis on research and development, the company has developed a range of dewatering pumps tailored specifically for the rigorous demands of the mining sector. Their pumps feature robust construction using high-strength alloys and abrasion-resistant components, ensuring durability under harsh conditions.

Additionally, the company’s innovative pump designs incorporate modular components, allowing for easy maintenance and part replacement. This modularity significantly reduces downtime, enabling mining firms to maintain optimal productivity. The company also offers customized solutions, working closely with clients to design pumps that meet specific site requirements, including various flow rates, head capacities, and power configurations.

In addressing environmental concerns, the company has invested in developing energy-efficient pump models that lower power consumption without compromising performance. By utilizing advanced hydraulic engineering and optimizing impeller designs, these pumps achieve higher efficiency rates, contributing to reduced operational costs and lower greenhouse gas emissions.

Safety is another cornerstone of the company’s approach. Their dewatering pumps are equipped with advanced monitoring systems that provide real-time data on operating conditions, enabling proactive maintenance and early detection of potential issues. This predictive maintenance capability enhances worker safety by preventing unexpected failures and facilitating timely interventions.

Mining industry experts acknowledge that such technological progress in dewatering pumps is instrumental in supporting the sector’s growth and sustainability objectives. As mines delve deeper and encounter more complex hydrogeological conditions, reliable and adaptable dewatering solutions become indispensable.

Furthermore, the integration of digital technologies, including IoT sensors and smart controls, is paving the way for smarter mine water management. These innovations enable remote monitoring and operation, reducing the need for personnel to work in hazardous environments and allowing managers to make data-driven decisions.

Looking ahead, ongoing collaboration between pump manufacturers and mining companies is expected to drive further enhancements. Focus areas include the development of pumps capable of handling more corrosive or sediment-laden water, improved energy recovery systems, and greater automation integration.

In summary, the evolution of dewatering pumps signifies a major leap forward in mining technology. Through engineering innovation, customer-focused customization, and a commitment to sustainability and safety, leading manufacturers are delivering solutions that meet the complex demands of modern mining operations. These advancements not only enhance operational efficiency but also contribute to safer and more environmentally responsible mining practices worldwide.

---

**About the Company**

The company, with decades of expertise in fluid machinery engineering, excels in designing and manufacturing a comprehensive range of pumps and related systems. With a global footprint and customer-oriented approach, the company delivers cutting-edge solutions tailored to diverse industrial sectors, including mining, water treatment, oil and gas, and construction.

Committed to innovation and quality, the company leverages advanced materials, precision manufacturing, and digital technologies to produce pumps that stand up to the most demanding environments. Their product portfolio includes centrifugal pumps, submersible pumps, sludge pumps, and specialized dewatering pumps engineered for efficiency, durability, and ease of maintenance.

Driven by a mission to improve operational performance and sustainability for clients worldwide, the company combines technical expertise with responsive service and support. Their collaborative project approach ensures that each solution is optimized for specific applications, helping clients overcome unique challenges and achieve their business goals.

With a strong emphasis on environmental responsibility, the company continually develops energy-saving products and promotes best practices in pump application and maintenance. Their dedication to safety, reliability, and customer satisfaction positions them as a trusted partner in advancing global industries, including the mining sector.

Company News & Blog

Bombas Slurry: The Latest Advancements in Slurry Pump Technology

AH Bombs Slurry, a leading company in the slurry pumping industry, has made a significant breakthrough with its latest product innovation. The company has successfully developed a new range of slurry pumps that are set to revolutionize the industry with their advanced technology and superior performance.AH Bombs Slurry has been at the forefront of slurry pumping technology for over two decades, and their commitment to innovation and excellence has positioned them as a market leader in the industry. The company has a proven track record of delivering high-quality and reliable products, and their latest innovation is set to further solidify their position in the market.The new range of slurry pumps developed by AH Bombs Slurry features cutting-edge technology that sets them apart from traditional pumps. These pumps are specifically designed to handle the most demanding slurry applications, providing enhanced efficiency, durability, and performance. The company's team of engineers and experts have worked tirelessly to create a product that meets the evolving needs of the industry, and the result is a range of pumps that deliver unparalleled performance and reliability.One of the key features of the new range of pumps is their enhanced wear resistance, which allows them to withstand the abrasive nature of slurry and maintain their performance over an extended period. This is a significant advancement in slurry pumping technology, as traditional pumps often suffer from wear and tear, resulting in reduced efficiency and increased maintenance costs. With the new pumps from AH Bombs Slurry, customers can expect reduced downtime and lower operating costs, making them a highly cost-effective solution for their slurry pumping needs.In addition to their superior wear resistance, the new pumps also incorporate state-of-the-art hydraulic design and materials to maximize efficiency and minimize energy consumption. This not only reduces the environmental impact of slurry pumping operations but also lowers the overall operational costs for customers. The pumps are also equipped with advanced sealing technology to prevent leakage and ensure seamless operation, even in the most challenging conditions.AH Bombs Slurry is committed to delivering exceptional value to its customers, and the new range of pumps is a testament to this commitment. The company understands the unique requirements of slurry pumping applications and has developed a product that addresses these challenges with unmatched performance and reliability.The new range of pumps from AH Bombs Slurry is already generating excitement in the industry, and the company has received a significant number of inquiries from customers eager to experience the benefits of this groundbreaking technology. With their reputation for delivering high-quality products and unparalleled customer service, AH Bombs Slurry is well-positioned to capitalize on the success of their latest innovation and further establish themselves as a dominant force in the slurry pumping industry.As the demand for superior slurry pumping solutions continues to grow, AH Bombs Slurry is poised to meet the needs of customers with their innovative and reliable products. The company's dedication to excellence and continuous improvement ensures that they will remain at the forefront of the industry, driving innovation and setting new standards for performance and reliability in slurry pumping technology.

Read More

Top Pump Parts for Efficient and Reliable Equipment Performance

Pump Parts, a leading supplier of industrial pump components, recently announced the release of their new and improved pump parts line. These high-quality parts are designed to enhance the performance and reliability of industrial pumps across a wide range of applications.With over 20 years of experience in the industry, Pump Parts has built a reputation for delivering innovative and reliable solutions for pump maintenance and repair. Their team of experienced engineers and technicians are dedicated to developing and producing the highest quality pump parts on the market.The new line of pump parts is the result of extensive research and development, aimed at meeting the evolving needs of industrial pump users. These parts are engineered to deliver superior performance and durability, even in the most demanding operating conditions.One of the key features of the new pump parts line is their enhanced efficiency and performance. With advanced materials and manufacturing processes, these parts are designed to minimize wear and tear, resulting in longer equipment life and reduced maintenance costs for pump operators.Additionally, Pump Parts has prioritized ease of installation and compatibility with a wide range of pump models. This ensures that their parts can be seamlessly integrated into existing pump systems, minimizing downtime and maximizing productivity for their customers.In addition to their commitment to quality and performance, Pump Parts also takes pride in their dedication to environmental responsibility. All of their pump parts are manufactured using sustainable practices and materials, ensuring minimal impact on the environment. This aligns with their company values and commitment to promoting sustainable solutions in the industrial sector.Furthermore, Pump Parts offers comprehensive customer support and technical assistance to ensure that their customers are able to maximize the benefits of their products. Their team of experts is available to provide guidance on part selection, installation, and ongoing maintenance, enabling their customers to get the most out of their investment in pump parts."We are excited to introduce our new line of pump parts, which represents a significant advancement in pump technology," said [Company CEO]. "Our team has worked tirelessly to develop these parts, utilizing the latest advancements in engineering and materials to deliver superior performance and reliability. We are confident that these parts will provide immense value to our customers, helping them achieve optimal pump performance and minimize downtime."Pump Parts is poised to continue making an impact in the industrial pump industry with their commitment to excellence and innovation. Their new line of pump parts is a testament to their dedication to meeting the needs of their customers and providing reliable solutions for the industrial sector. With their track record of success and commitment to customer satisfaction, Pump Parts is well-positioned to continue leading the way in the pump parts market.

Read More

High-Performance Slurry Pump Impeller for Efficient Material Handling

Certainly! Please provide the news content about the Slurry Pump Impeller and the company introduction you'd like me to incorporate. Once I have those details, I can craft an 800-word news article for you.

Read More

Top-quality Centrifugal Pump Manufactured in China: Latest News

China Centrifugal Pump Launches New State-of-the-Art Pump TechnologyChina Centrifugal Pump, a leading manufacturer in the field of pump technology, has recently announced the launch of their latest innovation in centrifugal pump technology. This state-of-the-art pump, which boasts cutting-edge features and technology, is set to revolutionize the industry and set a new standard for efficiency and reliability.With a history of over 30 years, China Centrifugal Pump has been at the forefront of innovation in pump technology and has established itself as a trusted and reliable provider of high-quality pumps for a wide range of applications. The company has built a strong reputation for delivering pumps that are not only efficient and reliable, but also tailored to meet the specific needs of their customers.The new centrifugal pump, which has been in development for several years, represents a significant milestone for China Centrifugal Pump. The pump features a number of advanced technologies that are designed to optimize performance and maximize energy efficiency. In addition, the pump also incorporates features that enhance durability and minimize maintenance requirements, making it an ideal choice for a wide range of industrial and commercial applications.One of the key features of the new centrifugal pump is its innovative design, which has been carefully engineered to deliver maximum performance while minimizing energy consumption. This means that customers can expect to see significant cost savings over the long term, as the pump is designed to operate with minimal energy input, without compromising on performance.Furthermore, the pump also incorporates advanced monitoring and control systems, which allow for real-time monitoring of key performance metrics. This not only enhances operational efficiency, but also allows for proactive maintenance and troubleshooting, reducing downtime and maximizing productivity.China Centrifugal Pump has also placed a strong emphasis on reliability in the design and construction of the new pump. The pump is built using high-quality materials and components, and undergoes rigorous testing to ensure that it meets the highest standards for durability and performance. This means that customers can have confidence in the reliability of the pump, even in the most demanding applications.In addition to its technical features, the new centrifugal pump also offers a range of practical benefits for customers. The pump is designed for easy installation and maintenance, and is backed by a comprehensive support and service network from China Centrifugal Pump. This means that customers can expect timely and efficient support, ensuring that their pump operates at peak performance throughout its lifecycle.Overall, the launch of the new centrifugal pump from China Centrifugal Pump represents a significant advancement in pump technology. With its innovative design, advanced features, and focus on reliability and efficiency, the pump is set to make a major impact in the industry and provide customers with a superior pumping solution for a wide range of applications.As China Centrifugal Pump continues to lead the way in pump technology, the company is poised to maintain its position as a trusted and innovative provider of high-quality pumps for the global market. With a strong commitment to research and development, as well as a focus on meeting the evolving needs of its customers, China Centrifugal Pump is well positioned to continue setting new standards for pump technology in the years to come.

Read More

High-quality Slurry Pump Supplier for Your Industrial Needs

Slurry Pump Supplier Expands Product Line to Meet Growing Demand in Mining and Construction IndustriesIn response to the increasing demand for high-quality slurry pumps in the mining and construction industries, Slurry Pump Supplier has recently expanded its product line to offer a wider range of options for their customers. The company, which has been a leading supplier of slurry pumps for more than two decades, is committed to providing reliable and efficient solutions to meet the diverse needs of its clients.With a focus on innovation and customer satisfaction, Slurry Pump Supplier has invested in research and development to enhance the performance and reliability of its products. The company's dedication to quality and excellence has allowed it to build a strong reputation as a trusted partner for businesses in the mining and construction sectors.The new additions to Slurry Pump Supplier's product line include a variety of pumps designed to handle different types of materials and operating conditions. These pumps are engineered to deliver high efficiency and durability, making them ideal for the demanding environments common in mining and construction applications."We are excited to announce the expansion of our product line to better serve our customers' needs," said a spokesperson for Slurry Pump Supplier. "Our goal is to provide the most reliable and cost-effective solutions for the challenges our clients face in their operations. With our expanded range of slurry pumps, we are confident that we can meet the growing demands of the industry and continue to exceed our customers' expectations."In addition to offering a wider selection of pumps, Slurry Pump Supplier also provides comprehensive technical support and after-sales services to ensure that its customers get the most out of their equipment. The company's team of experienced engineers and technicians are available to assist with installation, maintenance, and troubleshooting, helping clients minimize downtime and maximize productivity.Slurry Pump Supplier's dedication to customer support is a key part of its commitment to delivering complete solutions that address the specific needs of each client. By understanding the unique challenges facing businesses in the mining and construction industries, the company is able to provide tailored recommendations and ongoing assistance to help its customers achieve their operational goals.With its expanded product line and unwavering focus on customer satisfaction, Slurry Pump Supplier is well-positioned to continue meeting the evolving needs of the mining and construction industries. The company's ability to offer reliable, high-performance slurry pumps, coupled with its commitment to technical support and service, sets it apart as a valuable partner for businesses looking to optimize their operations.As the demand for slurry pumps continues to grow in the mining and construction sectors, Slurry Pump Supplier remains dedicated to being at the forefront of innovation and excellence in the industry. The company's continued investment in product development and customer support underscores its commitment to providing the best possible solutions for its clients, ensuring that they can rely on Slurry Pump Supplier for all their slurry pumping needs.

Read More

Sure! Please provide the original SEO title you want me to rewrite by removing the brand name.

Certainly! Please provide the news content for the Performance Test and the company introduction you would like me to use, and I will compose the 800-word news article for you.

Read More

Unlock the Potential of Quarrying Applications: A Comprehensive Guide

Title: Sustainable Quarrying Application Revolutionizes the Mining IndustryIntroduction:In today's rapidly advancing world, the mining industry plays a critical role in supporting various sectors and meeting the growing demand for natural resources. However, traditional quarrying practices often have a negative impact on the environment, affecting landscapes, habitats, and communities. To address these concerns, {Company Name}, a leading innovator in sustainable solutions, has introduced a cutting-edge quarrying application that aims to revolutionize the mining industry by minimizing its environmental footprint while maximizing efficiency and productivity.Body:1. Importance of Sustainable Quarrying:Sustainable quarrying practices are essential to ensure the long-term viability of the mining industry. By adopting environmentally responsible approaches, mining companies can reduce their carbon footprint, preserve biodiversity, and mitigate negative social and economic impacts. Recognizing the significance of sustainable quarrying, {Company Name} has developed a comprehensive application that integrates technology, innovation, and expert knowledge to provide an eco-friendly solution to the mining sector.2. Overview of {Company Name} and its Expertise:With years of industry experience, {Company Name} has emerged as a pioneer in providing sustainable solutions for the mining and extraction industry. By leveraging cutting-edge technology and adopting a holistic approach, the company has successfully developed innovative applications that optimize operations, minimize environmental harm, and maximize returns on investment.3. Features and Benefits of the Quarrying Application:The quarrying application developed by {Company Name} leverages advanced technologies such as artificial intelligence, machine learning, and remote sensing to revolutionize conventional mining practices. Some of its key features and benefits include:- Real-time Monitoring and Analysis: The application enables continuous monitoring and analysis of mining activities, ensuring prompt detection of potential environmental hazards, such as air and water pollution. This proactive approach allows for timely interventions, reducing any negative impact.- Resource Optimization: By utilizing sophisticated algorithms and predictive modeling, the application assists mining companies in optimizing resource allocation, reducing energy consumption, and minimizing waste generation. This not only contributes to sustainability but also enhances cost-effectiveness.- Tailings Management: The application focuses on efficient tailings management, helping mining companies adhere to strict environmental regulations. By minimizing the use of hazardous materials and incorporating sustainable disposal techniques, the application ensures responsible waste management practices.- Community Engagement: Alongside environmental considerations, the application also emphasizes community engagement. It provides various tools to enable effective communication and collaboration between mining companies and local communities, ensuring transparency and shared benefits.4. Successful Application Implementation and Case Studies:Several mining companies have already implemented the quarrying application developed by {Company Name}, resulting in significant improvements in sustainability and overall operational efficiency. These success stories serve as testimonials for the wider mining industry, highlighting the tangible benefits of embracing sustainable practices and technology-driven solutions.5. Future Prospects and Impacts:As the global focus on sustainability intensifies, the mining industry is experiencing increasing pressure to adhere to stringent environmental standards. {Company Name}'s quarrying application presents a promising solution to meet these growing demands. By minimizing the ecological footprint and enhancing operational efficiency, the application enables mining companies to maintain their social license to operate, improve profitability, and contribute to a more sustainable future.Conclusion:{Company Name}'s revolutionary quarrying application exemplifies the potential of technology-driven solutions to transform traditional mining practices. By prioritizing sustainability, the application paves the way for a more responsible and efficient mining industry that minimizes its environmental impact while meeting the rising demand for natural resources. With continued innovation and widespread adoption, the mining sector can become a champion for sustainable resource extraction, ensuring a better future for generations to come.

Read More

Ultimate Guide to Slurry Pump Volute Liner: Everything You Need to Know

[Company] is renowned for its high-quality slurry pumps and parts, and their latest innovation, the Slurry Pump Volute Liner, is set to revolutionize the industry. The company has been a leader in the manufacturing of slurry pumps and parts for over 20 years, and their commitment to innovation and quality has earned them a reputation as a trusted supplier in the industry.The Slurry Pump Volute Liner is designed to significantly improve the performance and durability of slurry pumps. It is made from high-quality materials and is precision-engineered to deliver optimal efficiency and reliability. The innovative design of the volute liner ensures smooth flow and minimal turbulence, which results in reduced energy consumption and lower operating costs. Additionally, the robust construction of the volute liner enhances the durability of the slurry pump, making it ideal for use in challenging operating environments."We are thrilled to introduce the Slurry Pump Volute Liner to the market," said [Company]'s CEO. "Our team has worked tirelessly to develop a product that not only meets but exceeds the expectations of our customers. We are confident that the Volute Liner will deliver exceptional performance and reliability, setting a new standard for slurry pump technology."The Slurry Pump Volute Liner is suitable for a wide range of applications, including mining, mineral processing, and industrial processes. Its versatile design allows for easy installation and compatibility with various types of slurry pumps, making it a cost-effective solution for businesses looking to enhance the performance of their pumping systems.In addition to the Slurry Pump Volute Liner, [Company] offers a comprehensive range of slurry pump parts and accessories, including impellers, casings, and shaft seals. All of their products are manufactured to the highest standards, ensuring exceptional performance and longevity.In line with their commitment to customer satisfaction, [Company] provides expert technical support and personalized service to assist customers in selecting the right products for their specific requirements. Their team of experienced engineers and technicians is dedicated to helping customers optimize their pumping systems and maximize operational efficiency.As a leading supplier in the industry, [Company] has established a global presence, serving customers in over 50 countries. Their commitment to quality, innovation, and customer satisfaction has earned them a loyal customer base and a reputation for excellence.The introduction of the Slurry Pump Volute Liner represents [Company]'s ongoing dedication to advancing the capabilities of slurry pump technology and providing innovative solutions to meet the evolving needs of their customers. With a focus on quality, reliability, and performance, [Company] continues to set the standard for excellence in the slurry pump industry.Customers can expect the Slurry Pump Volute Liner to deliver outstanding performance, durability, and cost-effectiveness, making it an indispensable component of their pumping systems. As [Company] continues to push the boundaries of slurry pump technology, customers can look forward to even more innovative solutions that will further enhance the efficiency and reliability of their operations.

Read More

Slurry Pumps: The Latest Breakthrough in Durable and Efficient Mining Equipment

Weir Enhances Slurry Pump Performance with Innovative TechnologyLeading global engineering company, Weir, is revolutionizing the slurry pump industry with its cutting-edge technology and superior product offerings. With a rich history of over 150 years, Weir has established itself as a trusted and reliable partner in delivering innovative solutions to customers worldwide. Through its commitment to research and development, the company continues to set new standards in slurry pump performance and efficiency.Weir's extensive range of slurry pumps is designed to handle the most demanding applications across various sectors, including mining, oil and gas, and the industrial sector. Backed by extensive research and development, these pumps have been engineered to withstand abrasive and corrosive materials, thus ensuring long-lasting performance in harsh operating conditions.The company's dedication to innovation is reflected in its continuous pursuit of advanced technologies. Weir's slurry pumps incorporate state-of-the-art features that improve efficiency and reduce maintenance costs. For example, the incorporation of advanced hydraulic designs allows for greater energy savings while delivering higher flow rates. By optimizing efficiency, Weir's pumps help customers maximize their productivity and minimize operational costs.The use of advanced materials also sets Weir pumps apart from the competition. By utilizing high-quality alloys and wear-resistant materials, Weir's slurry pumps offer exceptional durability and prolonged service life. This ensures reduced downtime and maintenance, resulting in increased operational efficiency for customers.Furthermore, Weir is committed to sustainability and minimizing its environmental impact. The company's slurry pumps are designed to minimize water and energy consumption, resulting in a more sustainable pumping solution. Weir recognizes the importance of reducing carbon emissions and actively develops products that help customers in their journey toward achieving environmental sustainability goals.In addition to its technological advancements, Weir's commitment to customer satisfaction sets it apart in the industry. The company provides comprehensive aftermarket support, offering spare parts, maintenance services, and technical assistance to ensure uninterrupted operation of its slurry pumps. Weir's global network of service centers ensures prompt support and quick response times, minimizing downtime for customers.Weir's dedication to providing unmatched slurry pump solutions has led to its recognition as a trusted partner for many prestigious projects worldwide. The company's pumps have been deployed in major mining operations, helping customers efficiently process and transport minerals. Weir's pumps have also played a vital role in the oil and gas sector, where they have handled harsh drilling and production environments. The reliability and performance of Weir's pumps have earned the company a reputation for excellence in the industry.Looking ahead, Weir is committed to ongoing innovation and collaboration with customers to develop tailored solutions that meet their specific needs. The company's research and development efforts will continue to focus on enhancing pump performance, reducing energy consumption, and improving sustainability. Weir aims to further strengthen its position as a global leader in slurry pump technology by delivering reliable, efficient, and sustainable solutions for customers across various industries.In conclusion, Weir is revolutionizing the slurry pump industry with its advanced technology and commitment to innovation. Through its cutting-edge hydraulic designs and utilization of high-quality materials, Weir's pumps offer superior performance and durability. The company's dedication to sustainability and customer satisfaction further sets it apart from competitors. With a rich history and a global presence, Weir is well-positioned to continue leading the industry and providing tailored solutions for customers around the world.

Read More

Highly Efficient Gravel Pumps for Mining and Construction Needs

Gravel Pumps: A Key Component in Dredging OperationsDredging operations are an essential part of infrastructure development, land reclamation, and environmental remediation projects. One of the key components in these operations is the gravel pump, which plays a crucial role in the extraction and transportation of sediment and other materials from underwater locations. In this article, we will explore the significance of gravel pumps in dredging operations and shed light on their importance in the construction and maintenance of waterways and coastal areas.Gravel pumps are high-powered, heavy-duty pumps designed to handle abrasive materials such as sand, gravel, and silt. These pumps are typically used in dredging operations to remove sediment and debris from riverbeds, lakes, and coastal areas. The extracted materials are then transported to a designated location for disposal or further processing.One company that has been at the forefront of gravel pump technology is {}. With over 30 years of experience in the design, manufacturing, and distribution of dredging and mining equipment, {} has established itself as a leading provider of high-quality pumps and related accessories. The company's gravel pumps are known for their robust construction, efficient performance, and durability, making them the go-to choice for dredging contractors and mining companies worldwide.The {} gravel pump series is specifically designed for handling abrasive materials in challenging dredging environments. These pumps are equipped with heavy-duty components, including wear-resistant impellers, liners, and casings, to ensure reliable performance in demanding applications. In addition, {} offers a range of pump sizes and configurations to cater to different dredging requirements, ensuring that customers can find the right solution for their specific needs.The company's commitment to innovation and continuous improvement is evident in its ongoing investment in research and development. By leveraging the latest technology and engineering advancements, {} strives to enhance the performance and efficiency of its gravel pumps, allowing customers to achieve higher productivity and lower operating costs. Furthermore, the company places a strong emphasis on quality control and product testing to ensure that its pumps meet the highest standards of reliability and durability.In addition to its extensive range of gravel pumps, {} also provides a comprehensive suite of support services to assist customers throughout the lifecycle of their equipment. This includes technical consultation, installation and commissioning support, maintenance and repair services, and spare parts availability. By offering end-to-end solutions, {} aims to empower its customers to maximize the performance and longevity of their dredging equipment.The company's dedication to customer satisfaction and industry leadership has earned it a solid reputation in the global dredging and mining markets. With a strong presence in more than 50 countries, {} has established a network of distribution partners and service centers to ensure prompt and reliable support for its customers worldwide. This extensive reach and customer-focused approach have made {} a trusted partner for many organizations involved in dredging and mining activities.In conclusion, gravel pumps play a critical role in dredging operations, enabling the efficient extraction and transport of sediment and other materials from underwater locations. As a leading provider of dredging and mining equipment, {} has been a driving force in the development of gravel pump technology, offering high-performance solutions that meet the demanding requirements of the industry. With a strong focus on innovation, quality, and customer support, {} continues to set the benchmark for excellence in the global dredging and mining sector.

Read More