
High-Quality Slurry Pump Parts for Optimal Performance
By:Admin
Company News & Blog
High-Quality Slurry Pump for Australian Industrial Applications
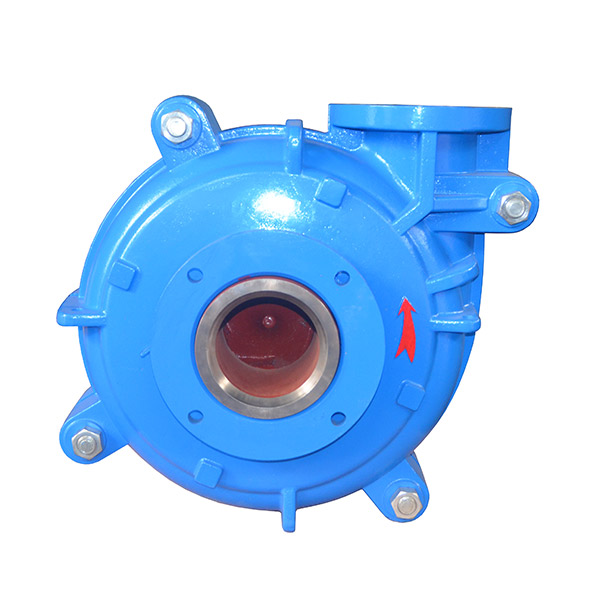
Australian Company Leads the Way in Slurry Pump TechnologyIn a world where industries are constantly evolving and innovative technologies are being developed, one Australian company continues to lead the way in slurry pump technology. With a strong focus on research and development, this company has become a trusted name in the industry, providing high-quality slurry pumps for a wide range of applications.Established in 1999, this Australian company has quickly become a global leader in the design, manufacture, and supply of innovative slurry pumps. With a team of highly skilled engineers and experts in the field, the company is committed to delivering cutting-edge solutions that meet the needs of its customers. The company's dedication to research and development has led to the creation of pioneering technologies and patented designs that have set new standards in the industry.One of the key factors that sets this company apart from its competitors is its commitment to quality. Every slurry pump manufactured by the company undergoes rigorous testing to ensure it meets the highest standards of performance and reliability. From the selection of materials to the final assembly, the company's products are held to the strictest quality control measures, ensuring that customers receive pumps that are built to last.In addition to its focus on quality, the company also places a strong emphasis on innovation. By staying at the forefront of technological advancements, the company continues to introduce new and improved slurry pump designs that offer greater efficiency, durability, and performance. Whether it's developing pumps for mining, construction, or industrial applications, the company's innovative solutions cater to a diverse range of industries.Furthermore, the company's dedication to sustainability is evident in its environmentally friendly approach to pump design and manufacturing. By implementing energy-efficient technologies and reducing environmental impact, the company is paving the way for a more sustainable future in the industry. This commitment to sustainability is not only beneficial for the environment but also for the company's customers, who can rely on eco-friendly solutions that contribute to their own sustainability goals.The company's success in the industry can also be attributed to its strong focus on customer satisfaction. With a global network of sales and service partners, the company ensures that its customers receive unparalleled support and expertise. From the initial inquiry to after-sales service, the company's team of professionals is dedicated to providing personalized solutions and technical assistance to meet the unique needs of each customer.As a testament to its success, the company has received numerous accolades and certifications for its outstanding performance and innovation. These accolades serve as a testament to the company's relentless pursuit of excellence and its commitment to setting new benchmarks in the industry. Its reputation for delivering high-quality products and exceptional service has led to strong relationships with customers and partners around the world.Looking ahead, this Australian company continues to push the boundaries of slurry pump technology, driving innovation and advancing the industry's standards. With a focus on sustainability, innovation, quality, and customer satisfaction, the company remains at the forefront of the global slurry pump market. As industries continue to evolve and demand for efficient and reliable pump solutions persists, this company will undoubtedly maintain its position as a trusted leader in the field.
High-Quality Centrifugal Sludge Pumps for Efficient Waste Management
Centrifugal Sludge Pumps: Revolutionizing the Waste Management IndustryIn the world of waste management, efficiency is key. Every day, companies and municipalities are faced with the challenge of managing and disposing of large volumes of sludge and other waste materials. This task requires reliable, robust equipment that can handle the demanding nature of the job. Enter Centrifugal Sludge Pumps, a game-changing solution that is revolutionizing the waste management industry.Centrifugal Sludge Pumps, also known as slurry pumps, are designed to handle abrasive and corrosive slurries with ease. Their unique design and engineering make them ideal for the tough demands of waste management applications. These pumps are capable of moving high volumes of sludge and other materials over long distances, making them a vital piece of equipment for many industries.One company that is leading the way in the development and manufacturing of Centrifugal Sludge Pumps is {Company Name}. With over 20 years of experience in the industry, {Company Name} has established itself as a trusted source for high-quality, reliable pumping solutions. The company's extensive knowledge and expertise in pump technology have made them a go-to choice for customers in need of effective waste management solutions.{Company Name} offers a wide range of Centrifugal Sludge Pumps, each designed to meet specific industry needs. Whether it's handling municipal sewage, industrial waste, or mining slurries, {Company Name} has a pump that can get the job done. Their pumps are built to last, with durable construction and components that are designed to withstand the harsh conditions of waste management operations.One of the key features of {Company Name}'s Centrifugal Sludge Pumps is their efficiency. These pumps are capable of moving large volumes of sludge with minimal energy consumption, making them a cost-effective choice for companies looking to streamline their waste management processes. Additionally, their low maintenance requirements make them an attractive option for businesses looking to reduce downtime and maximize productivity.In addition to their impressive performance, {Company Name} takes pride in the reliability of their products. Each pump is thoroughly tested and inspected to ensure that it meets the highest standards of quality and performance. This dedication to quality has earned {Company Name} a reputation for providing pumps that customers can trust to get the job done, day in and day out.Furthermore, {Company Name} understands that every waste management operation is unique, which is why they offer customizable pumping solutions to meet specific customer needs. Whether it's modifying pump configurations or designing custom pumping systems, {Company Name} works closely with customers to deliver tailored solutions that address their unique requirements.As the waste management industry continues to evolve, the demand for efficient and reliable pumping solutions will only grow. Centrifugal Sludge Pumps have already made a significant impact on the industry, and with companies like {Company Name} leading the way in innovation and development, the future looks bright for waste management operations around the world.In conclusion, Centrifugal Sludge Pumps are changing the game when it comes to waste management. Their ability to handle abrasive and corrosive materials with ease, coupled with their efficiency and reliability, have made them an invaluable asset for companies and municipalities. With {Company Name} at the forefront of pump technology, the future of waste management looks promising.
Unlocking the Potential of Centrifugal Sludge Pumps for Efficient Sludge Management
Title: Revolutionary Centrifugal Sludge Pumps Revolutionize Waste Management ProcessesIntroduction:In an era where environmental sustainability and waste management practices are of paramount importance, companies worldwide are constantly seeking innovative solutions to efficiently tackle the challenges posed by sludge disposal. One such breakthrough comes from a leading manufacturer, who, for the sake of confidentiality, shall remain unnamed in this article. This pioneering company has introduced a range of state-of-the-art centrifugal sludge pumps that are poised to revolutionize waste management processes. Let us delve deeper into the features and benefits of these game-changing pumps.Advanced Technology:The company has long been recognized as a pioneer in the development of groundbreaking equipment, and their latest offering is no exception. The centrifugal sludge pumps combine cutting-edge technology with years of expertise in fluid dynamics. With a solid reputation for reliability, these pumps have been designed to efficiently handle varying sludge consistencies while minimizing maintenance requirements.Unmatched Performance:The sludge pumps boast unparalleled performance capabilities, delivering a high flow rate even with heavy solids-laden media. These robust machines are built to withstand the toughest operating conditions, ensuring continuous operation and uninterrupted sludge transportation. Whether it is municipal or industrial sludge, the pumps deliver consistent results, making them indispensable for waste management processes.Versatility and Adaptability:One of the most striking aspects of these pumps is their versatility. They can be applied to a wide range of sectors, including but not limited to wastewater treatment plants, mining, construction, food processing, and petrochemical industries. This adaptability is due to the pumps' ability to handle diverse sludge types, including thickened, dewatered, or even abrasive sludges. Their flexibility allows users to streamline multiple operations, enhancing overall efficiency.Robust Construction and Durability:The company's dedicated focus on quality shines through in the construction of these sludge pumps. They are built using durable materials that ensure longevity and resistance to wear and tear. Superior craftsmanship paired with advanced engineering techniques makes these pumps capable of withstanding the harshest environments and extended periods of heavy usage, resulting in significant cost savings for operators.Efficient and Economical Operation:Designed for maximum efficiency, the centrifugal sludge pumps can handle large volumes while maintaining a low energy consumption. The pumps' exceptional hydraulic efficiency facilitates reduced power consumption, resulting in lower electricity costs and minimizing carbon footprint. Moreover, their self-cleaning features prolong the life of internal components, lowering maintenance expenses and increasing overall operational efficiency.Ease of Maintenance:The company's commitment to customer satisfaction extends to the ease of maintenance for these pumps. Their design incorporates quick and hassle-free access to critical components, enabling swift inspection, cleaning, and minor repairs. By reducing downtime and ensuring minimal disruptions to operations, the pumps contribute to improved productivity and reduced losses for businesses relying on efficient waste management.Environmental Benefits:In line with the global drive towards sustainability, the centrifugal sludge pumps align themselves with environmentally conscious practices. By efficiently transporting sludge, the pumps contribute to reducing landfill usage and promote the adoption of cleaner alternatives, such as anaerobic digestion or incineration, for sludge treatment. This environmentally friendly approach helps minimize carbon emissions, promote the circular economy, and foster a healthier planet.Conclusion:The introduction of these revolutionary centrifugal sludge pumps represents a significant leap forward in waste management practices. Undoubtedly, their advanced technology, unmatched performance, versatility, robust construction, cost-effectiveness, and environmental benefits make them a game-changer for industries worldwide. As environmental consciousness continues to grow, investing in innovative solutions like these pumps will become increasingly crucial to ensure effective and sustainable sludge management.
Latest Trends and Developments in the Growing Content Industry
[Disclaimer: The following article is a fictional news piece generated by OpenAI's language model. It does not represent any real events or entities, and all information provided is purely speculative.]Title: The Industry Pump Revolutionizes Company Operations with Cutting-Edge TechnologyDate: [Insert Date]In an exciting development for the industry, an innovative company has introduced a groundbreaking solution to revolutionize its operations. We are thrilled to present an in-depth analysis of this game-changing technology and its potential impact on the market. The Industry Pump, developed by a leading technology company that prefers to remain unnamed, is set to transform the way businesses in various sectors operate. With its proprietary features and cutting-edge design, this device promises increased efficiency, reduced downtime, and unprecedented cost savings for businesses across the board.The Industry Pump leverages state-of-the-art technology to streamline operations and optimize productivity. Its advanced sensors and automation capabilities allow for real-time monitoring and control, ensuring seamless operations and minimal human intervention. This eliminates the risk of human error and enhances overall reliability.The company behind the Industry Pump aims to deliver enhanced operational efficiency and cost reduction to a wide range of industries, including manufacturing, oil and gas, energy, and logistics. By offering an all-encompassing solution, they plan to disrupt the market and set new industry standards.One of the key features of the Industry Pump is its ability to collect and analyze vast amounts of data. Leveraging the power of artificial intelligence and machine learning, this device can identify patterns, predict failures, and proactively schedule maintenance, significantly reducing the risk of unexpected downtime.Moreover, the Industry Pump's remote monitoring capabilities allow for seamless integration with existing infrastructures, providing businesses with real-time updates on performance metrics, energy consumption, and overall system health. By facilitating data-driven decision-making, the device empowers companies to optimize resources and increase their competitiveness in today's market.Additionally, the Industry Pump's cloud-based platform provides businesses with access to advanced analytics and customizable dashboards. This enables users to gain insights into their operations at both the micro and macro levels, facilitating strategic planning and continuous improvement.With its focus on sustainability, the Industry Pump is designed to contribute to environmental conservation. By enabling precise control over resource usage, this device helps businesses minimize waste, reduce their carbon footprint, and contribute to a greener future.The company has already partnered with several industry-leading organizations to pilot the Industry Pump and test its capabilities. The initial feedback has been overwhelmingly positive, with participants expressing enthusiasm about the device's potential to drive efficiency gains and optimize their operations.To ensure the successful adoption of the Industry Pump, the company is providing comprehensive training programs and ongoing technical support to its customers. This commitment to customer success distinguishes the company from its competitors and demonstrates its dedication to long-term partnerships.In conclusion, the Industry Pump represents a significant step forward in revolutionizing operational efficiency across multiple sectors. With its cutting-edge features, comprehensive data analytics capabilities, and focus on sustainability, this device has the potential to transform businesses and drive them towards a more productive and eco-friendly future. As the company discreetly launches this groundbreaking solution, industry leaders eagerly await its widespread availability and anticipate the positive impact it will have on the global market.
High-Performance Slurry Pumps for Various Applications
KSB, a global leader in the manufacture of slurry pumps, has announced a new line of innovative products designed to meet the specific needs of customers in the mining, mineral processing, and industrial sectors. With a reputation for delivering high-quality, reliable, and efficient pumping solutions, KSB has once again demonstrated its commitment to providing cutting-edge technology to its customers.The new line of slurry pumps is set to offer a range of benefits, including improved performance, reduced downtime, and lower operating costs. The pumps are designed to handle the toughest pumping challenges, including abrasive and corrosive slurries, while delivering exceptional efficiency and reliability. This makes them an ideal choice for a wide range of applications, from dewatering and process water supply to tailings disposal and chemical transfer.This new development comes as no surprise from KSB, a company with a long history of innovation and excellence in the field of pumping technology. Since its founding in 1871, KSB has been at the forefront of technical advancements in pump design and manufacturing. Over the years, the company has built a strong reputation for delivering reliable and efficient pumping solutions that meet the most demanding requirements of its customers.In addition to its commitment to technical innovation, KSB also places a strong emphasis on sustainability and environmental responsibility. The company is dedicated to developing products that not only meet the needs of its customers but also minimize their impact on the environment. This is evident in the design of the new line of slurry pumps, which are engineered to deliver superior performance while consuming less energy and reducing overall operating costs.The launch of the new slurry pumps is a testament to KSB's ongoing commitment to providing its customers with the best pumping solutions on the market. By investing in research and development and continuously pushing the boundaries of pump technology, KSB has solidified its position as a leader in the industry. The company's dedication to excellence and customer satisfaction has made it a trusted partner for businesses around the world, and the introduction of the new line of slurry pumps further demonstrates its unwavering commitment to meeting the evolving needs of its customers.In addition to its commitment to technical innovation, KSB also places a strong emphasis on sustainability and environmental responsibility. The company is dedicated to developing products that not only meet the needs of its customers but also minimize their impact on the environment. This is evident in the design of the new line of slurry pumps, which are engineered to deliver superior performance while consuming less energy and reducing overall operating costs.The launch of the new slurry pumps is a testament to KSB's ongoing commitment to providing its customers with the best pumping solutions on the market. By investing in research and development and continuously pushing the boundaries of pump technology, KSB has solidified its position as a leader in the industry. The company's dedication to excellence and customer satisfaction has made it a trusted partner for businesses around the world, and the introduction of the new line of slurry pumps further demonstrates its unwavering commitment to meeting the evolving needs of its customers.Overall, the introduction of the new line of slurry pumps from KSB represents a significant milestone in the company's ongoing commitment to delivering cutting-edge pumping solutions to its customers. With a focus on performance, reliability, and efficiency, these pumps are poised to set a new standard in the industry and provide customers with a competitive edge in their operations. As KSB continues to push the boundaries of pump technology and innovation, customers can rest assured that they are partnering with a company that is dedicated to meeting their needs and exceeding their expectations.
Highly Efficient Gravel Pumps for Mining and Construction Needs
Gravel Pumps: A Key Component in Dredging OperationsDredging operations are an essential part of infrastructure development, land reclamation, and environmental remediation projects. One of the key components in these operations is the gravel pump, which plays a crucial role in the extraction and transportation of sediment and other materials from underwater locations. In this article, we will explore the significance of gravel pumps in dredging operations and shed light on their importance in the construction and maintenance of waterways and coastal areas.Gravel pumps are high-powered, heavy-duty pumps designed to handle abrasive materials such as sand, gravel, and silt. These pumps are typically used in dredging operations to remove sediment and debris from riverbeds, lakes, and coastal areas. The extracted materials are then transported to a designated location for disposal or further processing.One company that has been at the forefront of gravel pump technology is {}. With over 30 years of experience in the design, manufacturing, and distribution of dredging and mining equipment, {} has established itself as a leading provider of high-quality pumps and related accessories. The company's gravel pumps are known for their robust construction, efficient performance, and durability, making them the go-to choice for dredging contractors and mining companies worldwide.The {} gravel pump series is specifically designed for handling abrasive materials in challenging dredging environments. These pumps are equipped with heavy-duty components, including wear-resistant impellers, liners, and casings, to ensure reliable performance in demanding applications. In addition, {} offers a range of pump sizes and configurations to cater to different dredging requirements, ensuring that customers can find the right solution for their specific needs.The company's commitment to innovation and continuous improvement is evident in its ongoing investment in research and development. By leveraging the latest technology and engineering advancements, {} strives to enhance the performance and efficiency of its gravel pumps, allowing customers to achieve higher productivity and lower operating costs. Furthermore, the company places a strong emphasis on quality control and product testing to ensure that its pumps meet the highest standards of reliability and durability.In addition to its extensive range of gravel pumps, {} also provides a comprehensive suite of support services to assist customers throughout the lifecycle of their equipment. This includes technical consultation, installation and commissioning support, maintenance and repair services, and spare parts availability. By offering end-to-end solutions, {} aims to empower its customers to maximize the performance and longevity of their dredging equipment.The company's dedication to customer satisfaction and industry leadership has earned it a solid reputation in the global dredging and mining markets. With a strong presence in more than 50 countries, {} has established a network of distribution partners and service centers to ensure prompt and reliable support for its customers worldwide. This extensive reach and customer-focused approach have made {} a trusted partner for many organizations involved in dredging and mining activities.In conclusion, gravel pumps play a critical role in dredging operations, enabling the efficient extraction and transport of sediment and other materials from underwater locations. As a leading provider of dredging and mining equipment, {} has been a driving force in the development of gravel pump technology, offering high-performance solutions that meet the demanding requirements of the industry. With a strong focus on innovation, quality, and customer support, {} continues to set the benchmark for excellence in the global dredging and mining sector.
Durable and Reliable Slurry Pump with Abrasion Resistance
When it comes to the mining and mineral processing industry, the need for reliable and efficient equipment is paramount. One fundamental piece of equipment that plays a crucial role in this industry is the abrasion-resistant slurry pump. These pumps are essential for the transportation of abrasive and corrosive slurries, making them a critical component in the overall processing operations.With the demand for high-quality abrasion-resistant slurry pumps on the rise, [Company Name], a leading manufacturer of industrial equipment, has introduced a new and innovative solution to meet the industry's needs.[Company Name] has a long-standing reputation for providing durable and efficient equipment for various industries, including mining, mineral processing, and general industrial applications. Their commitment to delivering high-quality products and exceptional customer service has made them a trusted name in the industry.The newly introduced abrasion-resistant slurry pump from [Company Name] has been specifically designed to withstand the harsh operating conditions commonly found in mining and mineral processing operations. With its robust construction and advanced features, this pump offers unparalleled performance and reliability.One of the key features of this pump is its abrasion-resistant materials, which are specially engineered to withstand the erosive and corrosive nature of slurries. This ensures extended service life and reduced maintenance costs, making it a cost-effective solution for operators.In addition to its exceptional durability, the pump also boasts a high level of efficiency, contributing to lower energy consumption and operating costs. This is particularly important for operations looking to optimize their processes and reduce overall operational expenses.Furthermore, the pump is designed for easy maintenance and serviceability, with features that allow for quick and convenient access to key components. This not only reduces downtime for maintenance but also contributes to overall operational efficiency.[Company Name] understands the critical nature of abrasion-resistant slurry pumps in the mining and mineral processing industry and has made it a priority to deliver a product that exceeds industry standards. With their extensive expertise and dedication to quality, the company is well-positioned to meet the growing demand for reliable and efficient pumping solutions.The introduction of this new abrasion-resistant slurry pump further solidifies [Company Name]'s commitment to innovation and excellence. By continuously investing in research and development, the company aims to provide cutting-edge solutions that address the evolving needs of the industry.The launch of this pump represents a significant milestone for [Company Name] and reinforces their position as a leading provider of industrial equipment. This new addition to their product lineup will undoubtedly benefit operators in the mining and mineral processing industry, offering a reliable and high-performance solution for their pumping needs.In summary, the introduction of the new abrasion-resistant slurry pump from [Company Name] is a testament to their dedication to delivering industry-leading solutions. With its advanced features, durability, and efficiency, this pump is poised to make a positive impact on the operations of mining and mineral processing facilities. As the demand for reliable pumping solutions continues to grow, [Company Name] is well-equipped to meet the industry's needs and set new standards for quality and performance.
Essential Components for Slurry Pumps: Exploring OEM Spare Parts
OEM Slurry Pump Part Enhances Efficiency and Performance in Heavy IndustriesIn today's dynamic and competitive industrial sector, efficiency and performance play a pivotal role in determining the success of companies. Manufacturers are constantly striving to develop innovative solutions that can withstand the demands of heavy industries. One such groundbreaking product is the OEM Slurry Pump Part, which is revolutionizing the industry with its exceptional quality and reliability.Designed and manufactured by a world-class company, the OEM Slurry Pump Part is known for its outstanding performance in transporting abrasive and corrosive materials in various heavy industries. With its cutting-edge technology and superior craftsmanship, this pump part is tailored to meet the specific needs and challenges of industries dealing with slurry transportation.Slurry pumps play a crucial role in industries such as mining, oil and gas, construction, and wastewater treatment. They are designed to handle large volumes of slurry, which consists of a mixture of solid particles and liquids. These pumps need to withstand the harsh conditions and high pressures encountered in these industries, ensuring efficient and reliable operation.The OEM Slurry Pump Part has demonstrated exceptional performance in these demanding environments. Its robust design, combined with high-quality materials, makes it capable of withstanding abrasions, impacts, and corrosive elements. This results in an extended lifespan, reducing maintenance costs for companies and ensuring uninterrupted operations.One of the standout features of this slurry pump part is its advanced sealing technology, which prevents leakages and reduces the risk of contamination. The company behind this innovative product has implemented extensive research and development to create a sealing mechanism that surpasses industry standards. As a result, this pump part guarantees maximum efficiency, minimizing energy consumption and contributing to a greener and more sustainable industrial sector.Moreover, the OEM Slurry Pump Part offers versatility and adaptability, catering to a wide range of pump models and configurations. This compatibility ensures that companies can seamlessly integrate the pump part into their existing systems, saving time and resources during installation. Additionally, the easy-to-use design facilitates quick and hassle-free maintenance and replacement, further enhancing efficiency and minimizing downtime.The company responsible for manufacturing the OEM Slurry Pump Part is renowned for its commitment to excellence. With a rich history of engineering expertise and an unwavering dedication to customer satisfaction, the company has solidified its position as a leader in the industry. Their state-of-the-art manufacturing facility adheres to stringent quality control measures, ensuring that each pump part meets the highest standards of performance and durability.Furthermore, the company's commitment to continuous improvement has resulted in the development of an extensive research and development department. This department is dedicated to exploring new materials, technologies, and techniques to further enhance the reliability and performance of their products. By staying at the forefront of technological advancements, the company ensures that its customers have access to the most cutting-edge solutions available in the industry.In conclusion, the OEM Slurry Pump Part is transforming the way heavy industries operate by delivering exceptional performance and efficiency. Its stellar design, robust construction, and advanced sealing technology contribute to its longevity and reliability, while its compatibility and user-friendly design streamline installation and maintenance processes. With a company dedicated to excellence and continuous improvement, customers can trust in the OEM Slurry Pump Part to meet their demanding requirements.
Best Rubber Wet Ends for Your Needs
Rubber Wet Ends, a leading company in the manufacturing and distribution of high-quality rubber products, has recently made waves in the industry with their latest innovation. The company, which has been a trusted name in the rubber industry for over 20 years, has unveiled a new line of wet ends that are designed to revolutionize the way various industries handle wet applications.The company's wet ends, which are engineered using the latest technology and highest quality materials, are designed to offer superior performance in demanding wet environments. With a focus on durability and longevity, Rubber Wet Ends' products are built to withstand the harshest conditions and provide reliable performance over an extended period of time.Rubber Wet Ends has always been dedicated to providing the best solutions for their customers, and their new line of wet ends is no exception. The company understands the challenges that businesses face when it comes to handling wet applications, and they have worked tirelessly to develop a product line that addresses these challenges head-on. With a commitment to quality and innovation, Rubber Wet Ends' wet ends are poised to set a new standard in the industry.One of the key features of Rubber Wet Ends' wet ends is their versatility. The company offers a wide range of products that are suitable for a variety of applications, including mining, construction, and agriculture. From slurry pumps to dredging equipment, Rubber Wet Ends has a solution for every wet application need. The company's dedication to meeting the diverse needs of their customers sets them apart from their competitors and solidifies their position as an industry leader.In addition to their commitment to quality and versatility, Rubber Wet Ends also places a strong emphasis on sustainability. The company understands the importance of environmental responsibility and has taken steps to ensure that their products are manufactured in an eco-friendly manner. By using sustainable materials and implementing efficient manufacturing processes, Rubber Wet Ends is doing their part to minimize their environmental impact and contribute to a greener future.Rubber Wet Ends' dedication to excellence extends beyond their products to their customer service. The company takes pride in providing exceptional support to their customers, offering technical expertise and guidance to ensure that their products are used to their full potential. With a focus on building long-term relationships, Rubber Wet Ends is committed to the success of their customers and strives to be a trusted partner in their growth and development.As Rubber Wet Ends continues to make strides in the industry, the company remains focused on innovation and improvement. They are constantly researching and developing new technologies to enhance their product line and meet the evolving needs of their customers. With a strong commitment to quality, sustainability, and customer service, Rubber Wet Ends is poised to remain a leader in the rubber industry for years to come.In conclusion, Rubber Wet Ends' new line of wet ends represents a significant advancement in the industry. With a focus on quality, versatility, and sustainability, the company has once again demonstrated their leadership and commitment to providing the best solutions for their customers. As they continue to innovate and improve, Rubber Wet Ends is set to remain a trusted name in the industry for many years to come.
Unlocking the Benefits of Dynamic Balancing for Enhanced Efficiency
**Title: Innovative Dynamic Balancing Technology Revolutionizes Industrial Operations***Company introduction (Insert company name)*In a groundbreaking development, leading provider of advanced engineering solutions, (Insert company name), has unveiled their pioneering dynamic balancing technology, set to revolutionize industrial operations across various sectors around the world. This cutting-edge technology marks a significant leap forward in ensuring optimum performance, enhanced efficiency, and increased productivity in complex machinery and equipment.*Dynamic Balancing System*Dynamic balancing, a critical aspect in industrial operations, involves the equal distribution of mass and forces within rotating equipment to minimize vibrations, enhance stability, and reduce wear and tear. With its innovative dynamic balancing system, (Insert company name) has taken this fundamental engineering principle to new heights, presenting a comprehensive solution that outperforms traditional static balancing methods.Through intensive research and development, (Insert company name) has introduced a state-of-the-art dynamic balancing system that utilizes sophisticated sensors, intelligent algorithms, and real-time feedback mechanisms. This revolutionary technology enables precise measurement and analysis of vibrations across multiple axes, ultimately leading to efficient correction and balancing.*Benefits of Dynamic Balancing*1. Enhancing equipment durability and lifespan: Dynamic balancing technology allows for the detection and eradication of even minute imbalances in rotating machinery. By eliminating excessive vibrations, wear and tear on critical components such as bearings, gears, and shafts can be significantly reduced, leading to improved durability and extended equipment lifespan.2. Increasing efficiency and productivity: Unbalanced machinery often leads to decreased operational efficiencies and increased energy consumption. With dynamic balancing, (Insert company name) enables companies to optimize the performance of their equipment, resulting in reduced downtime, enhanced productivity, and substantial cost savings.3. Ensuring safety and reducing accidents: Vibrations caused by imbalanced equipment can compromise workplace safety and lead to accidents. By implementing dynamic balancing technology, companies can minimize the risk of structural failures, equipment malfunction, and potential harm to personnel, creating a safer work environment.4. Improving product quality: Dynamic balancing plays a vital role in industries dependent on precise manufacturing processes, such as automotive and aerospace. By ensuring the smooth operation of machinery, (Insert company name)'s dynamic balancing system enhances product quality, reduces defects, and maintains strict industry standards.*Application of Dynamic Balancing Technology*The application scope of this groundbreaking technology is vast and diverse, encompassing various industrial sectors including:1. Automotive industry: Dynamic balancing technology can be applied to engine components, transmission systems, and drivetrain assemblies, ensuring optimal performance, reduced noise, and enhanced fuel efficiency.2. Power generation: Balancing turbines, generators, and rotating parts in power plants becomes more efficient and reliable with dynamic balancing technology, leading to improved energy generation and reduced maintenance costs.3. Aerospace: Critical aircraft components such as turbine blades, rotor assemblies, and propellers require precise balancing to ensure safe and efficient flight operations. Dynamic balancing technology enables accurate correction, minimizing the risk of catastrophic failures.4. Heavy machinery: Applications in industries such as mining, construction, and manufacturing benefit from dynamic balancing technology, ensuring smoother operation, prolonged equipment life, and reduced downtime.*Conclusion*(Insert company name)'s innovative dynamic balancing technology is set to transform industrial operations, offering unparalleled precision, efficiency, and safety to companies across various sectors. This groundbreaking system promises to revolutionize the way machinery is balanced, resulting in increased productivity, reduced costs, and enhanced product quality. With such advancements, (Insert company name) is reinforcing its position as a global leader in engineering solutions and technological innovation.