
Vertical Tank Slurry Pumps: Efficient Solutions for Industrial Applications
By:Admin
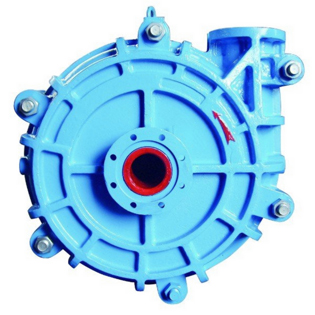
In recent developments within the industrial pump sector, vertical tank slurry pumps have emerged as a pivotal technology, revolutionizing the handling of abrasive and corrosive slurries across various industries. These pumps are designed to provide robust performance, operational efficiency, and longevity in challenging environments such as mining, chemical processing, and wastewater treatment.
Vertical tank slurry pumps are engineered to operate submerged within tanks, offering distinct advantages over traditional horizontal pumps. Their vertical configuration eliminates the need for a seal water system, reduces floor space requirements, and minimizes leakage risks. This design simplifies maintenance and contributes to improved safety standards in industrial settings.
One of the critical features of vertical tank slurry pumps is their capability to handle high concentrations of solids within fluids, making them ideal for slurry transportation. The pumps typically consist of durable materials such as high-chrome alloys and rubber linings, enhancing resistance to wear and corrosion. This ensures sustained performance in handling abrasive slurries, such as those found in mineral processing and dredging operations.
The adaptability of vertical tank slurry pumps extends to various industrial processes. In the mining sector, for instance, these pumps facilitate the effective movement of tailings and concentrate slurries, significantly reducing downtime and maintenance costs. Chemical plants utilize these pumps for transporting corrosive mixtures safely, while wastewater treatment facilities benefit from their ability to handle sludge efficiently without clogging or degradation.
Moreover, advancements in hydraulic design and impeller technology have further elevated the efficiency of vertical tank slurry pumps. These improvements contribute to lower energy consumption, enhanced throughput, and reduced operational costs. The modular design of these pumps also allows customization to meet specific process requirements, enabling companies to optimize their systems for varying flow rates and slurry densities.
The widespread adoption of vertical tank slurry pumps reflects a broader trend towards smarter, more reliable industrial equipment. Companies invested in pumping solutions emphasize sustainability and lifecycle cost savings, which vertical tank slurry pumps address by minimizing maintenance demands and extending service intervals.
With ongoing research and development, next-generation vertical tank slurry pumps are expected to integrate digital monitoring capabilities, allowing real-time performance tracking and predictive maintenance. This integration aligns with Industry 4.0 initiatives, promoting enhanced process control and operational transparency.
In summary, vertical tank slurry pumps represent a significant advancement in slurry handling technology, offering robust design, operational efficiency, and adaptability across multiple industries. Their ability to manage challenging slurry conditions reliably while reducing maintenance and operational costs positions them as a preferred solution in modern industrial applications. As industries continue to seek innovative pumping solutions, vertical tank slurry pumps exemplify the convergence of engineering excellence and practical functionality.
---
**About the Company**
Established with a commitment to engineering excellence, the company has developed a comprehensive range of industrial pumping solutions designed to meet the demanding needs of today’s industrial processes. Leveraging cutting-edge technology and a deep understanding of fluid dynamics, the company specializes in manufacturing durable, high-performance pumps tailored for slurry, mining, chemical, and wastewater applications.
The company’s portfolio spans vertical and horizontal slurry pumps, process pumps, and custom-engineered solutions, all designed to optimize operational efficiency and reliability. With a focus on innovation, quality, and customer satisfaction, the company supports its clients through every stage of the project lifecycle, from design consultation to after-sales service.
Adhering to international standards and employing rigorous quality control measures, the company ensures that each product delivers exceptional performance and longevity in the harshest environments. Its global network of technical experts and service centers provides timely support, minimizing downtime and enhancing productivity for clients worldwide.
Through continuous investment in research and development, the company remains at the forefront of pump technology, driving improvements in energy efficiency, wear resistance, and smart system integration. This commitment to innovation underscores its role as a trusted partner for industries seeking reliable and sustainable pumping solutions.
By focusing on customer-centric solutions and maintaining stringent quality benchmarks, the company continues to expand its footprint in the industrial pump market, contributing to safer, more efficient, and environmentally responsible operations across diverse industrial sectors.